Chemical Resistant Conveyor Belt
Custom chemical resistant conveyor belts for acids, alkalis and corrosive industrial materials.
Acid & Alkali Resistance • EP Fabric Options • Custom Compound & Dimensions
Product Overview
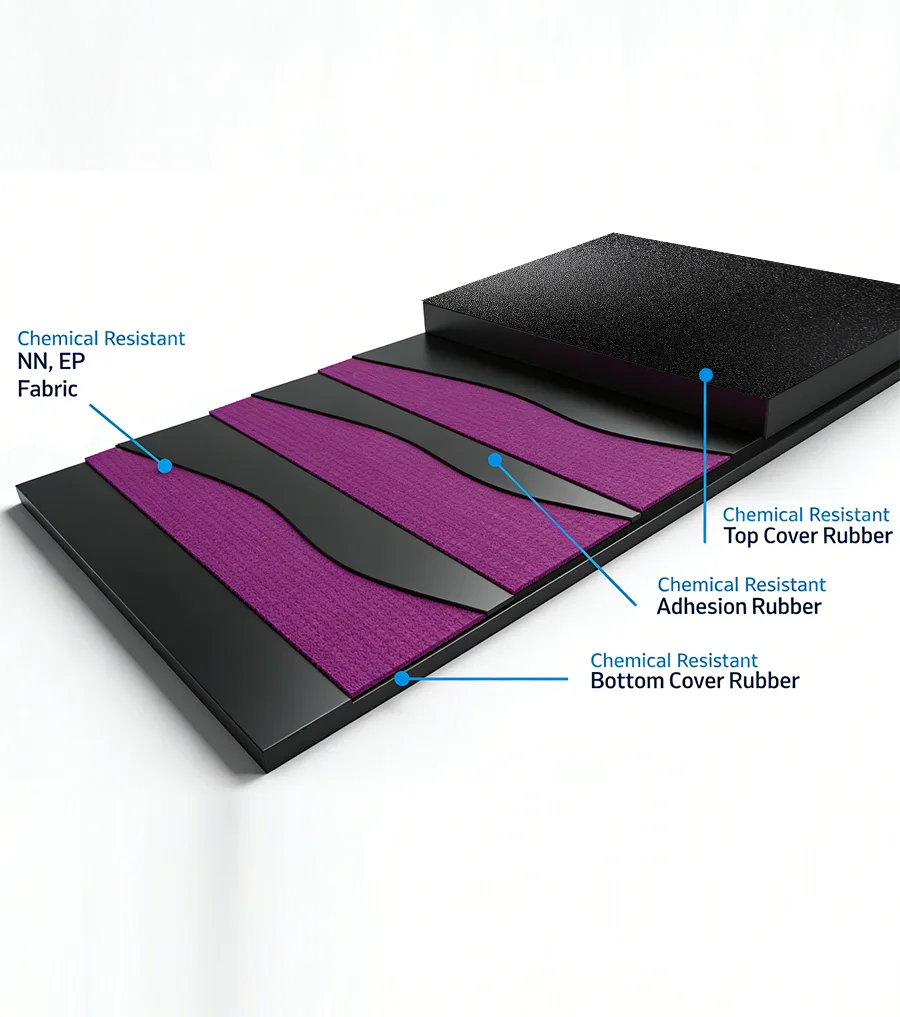
Chemical resistant conveyor belts are designed for handling corrosive materials in harsh industrial environments. They are made with special rubber compounds that resist chemical damage and protect the belt structure.
They are suitable for conveying materials containing acids, alkalis and other chemicals, and are widely used in chemical plants, fertilizer industries, mining and waste treatment systems.
Key Advantages

Excellent resistance to acid and alkali corrosion
Protects belt structure from chemical damage
Maintains stable performance in harsh environments
Suitable for chemical and industrial applications
Reliable and durable under corrosive conditions
Available in customized specifications for handling materials containing acids, alkalis and other chemicals, based on your project requirements.
Product Features & Capabilities
- Chemical Resistant Rubber Compound
- Specially developed to resist acid and alkali corrosion. Stable Physical Properties
- Maintains strength and flexibility under chemical exposure. Extended Service Life
- Reduces damage and degradation caused by corrosive materials. Wide Application Range
- Suitable for chemical plants, fertilizer production and mining industries. Multiple Construction Options
- Available with EP fabric and other reinforcement structures. Reliable Conveying Performance
- Ensures safe and stable transport of corrosive materials. Customizable Specifications
- Belt width, thickness and compound type can be tailored to requirements.
Chemical Resistant Conveyor Belt Applications
- Chemical plants and fertilizer production
- Mining and mineral processing
- Waste treatment and corrosive material handling
Chemical Resistant Conveyor Belt Customization
- Compound selected for the specific acid, alkali or chemical
- EP fabric and other reinforcement structures
- Custom belt width, thickness and compound type
Information Needed for a Quotation
Please provide the chemical or material name, concentration if available, belt dimensions, temperature and operating conditions. These details help JM Belt recommend a suitable configuration.
Chemical Resistant Conveyor Belt FAQ
What determines the correct chemical-resistant compound?
The chemical or material name, concentration, operating temperature and exposure conditions are required to select a suitable compound. Compatibility should be confirmed for the actual application.
Where is this product commonly used?
Typical applications include chemical plants and fertilizer production, mining and mineral processing, waste treatment and corrosive material handling.
What can be customized?
The compound for the specific acid, alkali or chemical, EP fabric or other reinforcement structure, belt width and thickness can be configured.
What should I include with my inquiry?
Please include the chemical or material name, concentration if available, belt dimensions, temperature and operating conditions.
Why Choose JM Belt?
- Professional manufacturer of heavy-duty conveyor belts
- Strict quality control and testing system
- Customized solutions for global clients
- Fast delivery and reliable after-sales service
Need a Reliable Acid and Alkali Resistant Conveyor Belt?
Contact us today for professional advice and competitive pricing.